Our well-equipped quality assurance laboratory conducts continuous mechanical, electrical, thermal, and chemical testing on 12 dedicated testing machines to guarantee absolute zero-defect delivery.
Our rigid raw material inspection, continuous in-process diameter & concentricity monitoring, and final functionality tests in our specialized Biratnagar laboratory ensure that every conductor meets international IEC 60317, IS 13730, and Nepal Standard (NS) certifications.
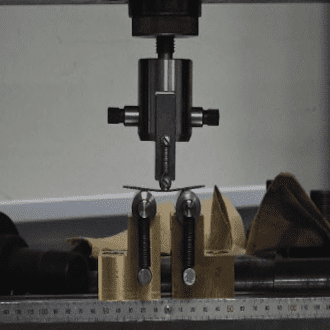
Evaluates the adhesion and flexibility of the enamel insulation film around a mandrel without peeling or microscopic surface cracking.
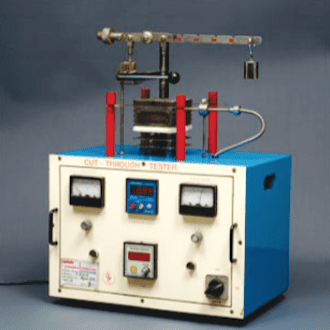
Measures the temperature at which the enamel insulation softens and flows under extreme mechanical pressure and heavy thermal stress.
High-precision digital gauge used to verify bare conductor diameter, enamel build thickness, and overall outside diameter to within 0.001 mm.
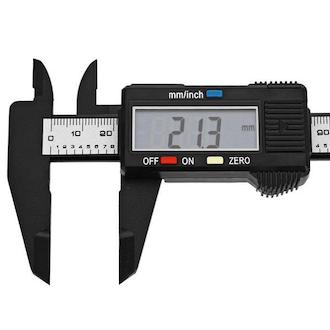
Precision caliper instrumentation to ensure exact cross-sectional dimensional accuracy for rectangular and flat copper strips.
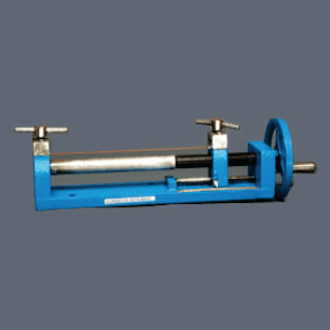
Measures the percentage of wire stretching before rupture to ensure optimum annealing softness and superior winding formability.
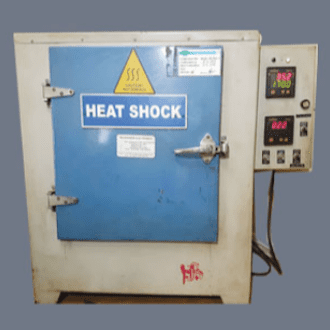
Oven chamber testing where wound samples are subjected to abrupt temperature spikes (up to 200°C) to verify film stability.
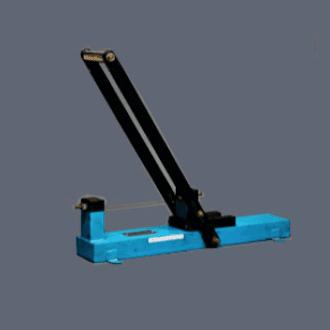
Simulates sudden high-speed mechanical tensile jerks during high-speed winding machine cycles to confirm elongation elasticity.
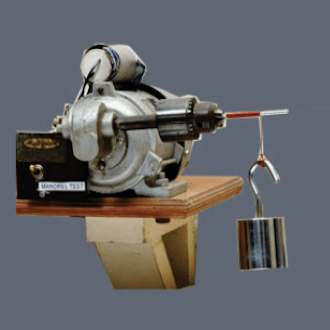
Precision winding apparatus that wraps wire around calibrated mandrels to inspect outer surface tension and coating cohesiveness.
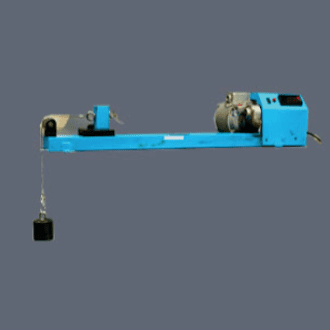
Tests bonding strength between copper core and insulation layer through calibrated rotational scraping forces.
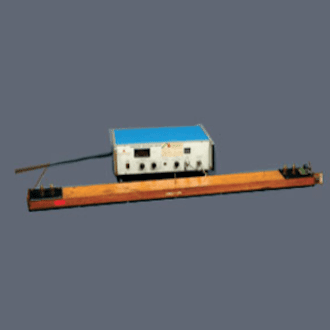
Measures electrical conductor resistance in ohms per kilometer with temperature coefficient compensation to guarantee >100% IACS.
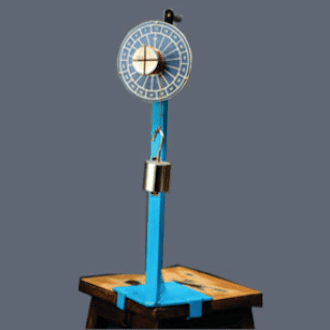
Measures the deflection angle and springback resilience of wound coils to guarantee tight, compact packing in motor armature slots.
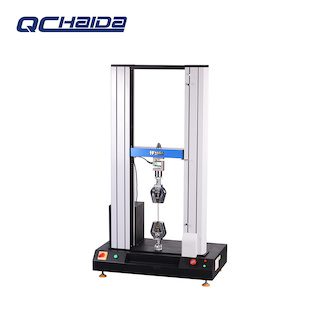
Heavy-duty universal hydraulic tensile testing machine designed to measure ultimate breaking stress and yield points across heavy conductors.
Click on either chart below to view high-resolution conversions for Standard Wire Gauge (SWG), bare wire diameters, and insulation parameters.
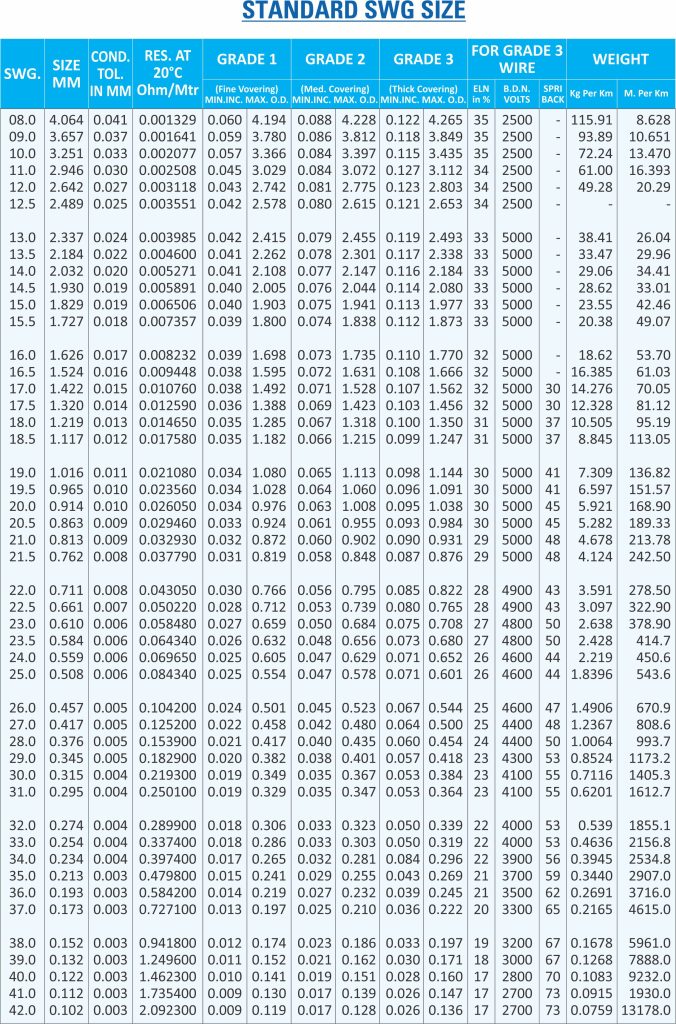
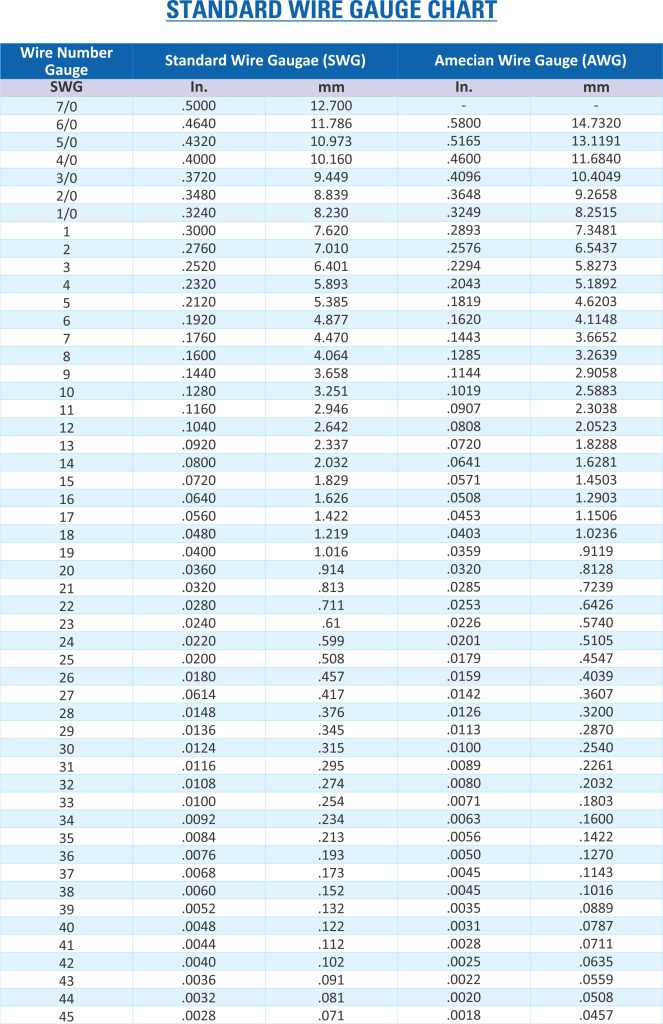
From continuous cast copper rods to precision spooled reels, each stage adheres to standardized industrial protocols.
Continuous cast electrolytic copper rods (99.99% purity) undergo spectroscopic analysis and surface defect inspection before entry into drawing mills.
Tungsten carbide and diamond dies draw the copper through multi-stage reduction steps to the exact target SWG gauge (from SWG 8 down to SWG 42).
Controlled-atmosphere electric annealing restores ductility. Computerized precision applicators apply multi-coat synthetic enamels baked in vertical ovens.
Each batch undergoes all 12 laboratory functionality tests (pinhole, resistance, breakdown, flexibility) before precision winding onto dynamic balance spools.